CHINAF's full-module smart factory solution spans seven core modules—intelligent R&D and manufacturing, production and scheduling, quality control, equipment O&M, logistics and warehousing, energy management, and an industrial-chain collaboration platform.
Built around digital twin and AI, it delivers full lifecycle digital R&D, centralized resource scheduling, lifecycle quality control, and plant-wide O&M and logistics-energy management. Connecting the entire R&D–production–sales chain, it enables R&D-production and production-supply collaboration for intelligent, efficient, green operations.
Smart Factory
Solution Introduction
Solution Introduction
Technical Features

Industrial Chain Collaboration Platform
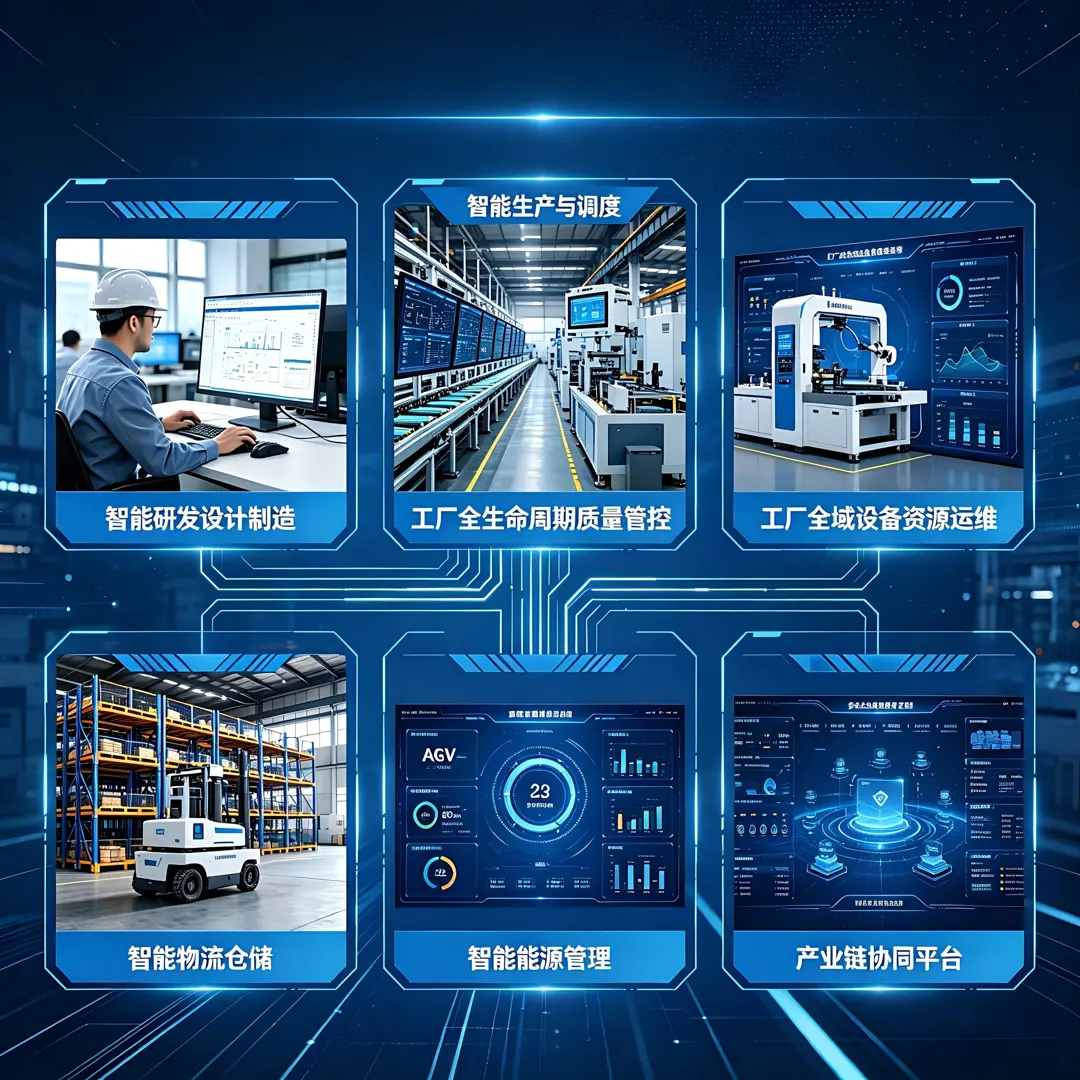
Relying on automated high-bay warehouses, AGV/AMR unmanned delivery, and intelligent inventory management, it achieves real-time material tracking, pull-based precise flow, and automatic sorting and distribution. It provides unmanned warehousing, intelligent distribution, and supply-chain visualization capabilities, optimizing warehousing and logistics efficiency.

Intelligent Equipment O&M
Based on multi-dimensional equipment operational data and AI fault-prediction models, it builds a predictive-maintenance and AR remote O&M system covering equipment-health assessment, fault prediction, and maintenance scheduling. It reduces unplanned downtime and improves O&M efficiency while lowering maintenance costs.

Intelligent Quality Control
Integrating AI online inspection, full-chain one-code-per-item traceability, and AI quality early-warning, it builds a closed-loop quality-control system. It realizes full-process quality traceability from raw materials to finished products and quality prediction with early warning, improves inspection efficiency, and achieves 100% in-process quality inspection with proactive defective-product prevention.

Intelligent Production and Scheduling
Relying on MES and process digital twins, through dynamic intelligent scheduling and adaptive process control, it achieves flexible production with transparent, traceable full-process production. It optimizes scheduling in real time, automatically adjusts process parameters, centrally schedules production resources, and maximizes resource utilization.
Intelligent R&D, Design and Manufacturing
Centered on digital twins, modular design, and simulation optimization, it builds a full-value-chain closed loop, realizing digital R&D across the product full lifecycle. It shortens the R&D cycle, improves part-reuse rate and product design performance, connects design and manufacturing, links production and supply-chain systems, and achieves R&D-production and production-supply collaboration.
Industrial-Chain Collaboration Platform
Connecting upstream and downstream data links, it integrates supplier collaboration, order collaboration, inventory sharing, quality linkage, and order-to-delivery full-process transparency. It achieves efficient collaboration across the production-sales and supply-demand full chains, shortens supply-chain response cycles, and supports flexible customized production.
Intelligent Energy Management
Conducting equipment-level real-time monitoring of plant-wide energy consumption across water, electricity, gas, and heat, and relying on AI energy-consumption optimization, carbon-emission management, and carbon-footprint tracking, it optimizes energy-use strategies, realizes refined energy-consumption control, and supports carbon reduction and carbon-neutrality monitoring and analysis.
Core Value
Full-Chain Collaboration
By connecting the full production-sales-R&D chain, it achieves efficient upstream-downstream collaboration, shortens supply-chain response cycles, supports flexible customization, and enhances core competitiveness.
Green and Energy-Saving
Through plant-wide refined energy-consumption control, it optimizes energy-use strategies, achieves carbon reduction, helps factories reach carbon-neutrality goals, and lowers energy costs.
Logistics Optimization
Through plant-wide intelligent logistics and warehousing, it improves storage-space utilization and logistics efficiency, reduces line-side inventory and labor costs, and enhances logistics safety.
Efficient Operation and Maintenance
Through plant-wide equipment predictive maintenance and AR remote O&M, it reduces unplanned downtime, lowers equipment maintenance costs, and improves equipment O&M efficiency and stability.
Controllable Quality
Through full lifecycle closed-loop quality control, it achieves 100% in-process inspection, precise traceability, and proactive defective-product prevention, ensuring stable product quality.
Production Optimization
Through centralized production-resource scheduling and flexible production, it improves overall equipment efficiency (OEE), on-time delivery rate, and order-fulfillment capability, realizes transparent and controllable full-process production, and maximizes resource utilization.
Efficient Research and Development
Through digital R&D across the product full lifecycle, it shortens the R&D cycle, improves design performance and part-reuse rate, achieves R&D-production collaboration, and reduces R&D costs.